
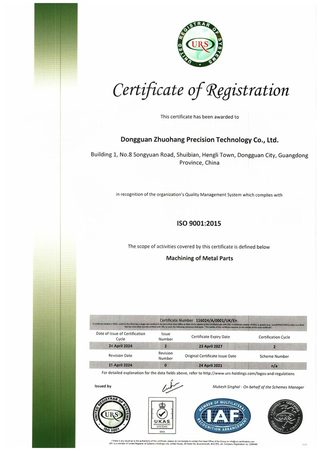
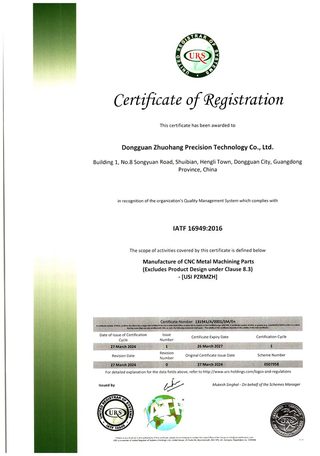
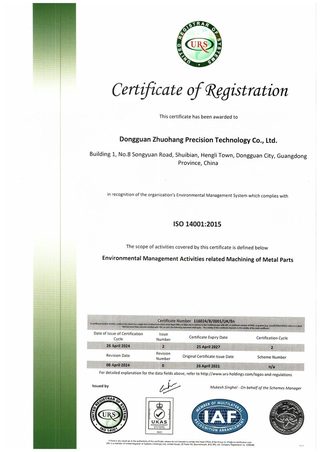
- Certifications — three standards, each with a verifiable certificate number.
- Metrology — CMMs and instruments an order of magnitude finer than the tolerance.
- SPC — control charts with Ppk ≥ 1.67 at the initial study on key characteristics.
- APQP/PPAP — process flow, control plan, PFMEA, and SPC as evidence.
- Traceability — one lot back to material, machine, operator, and result.
Which certifications should a quality audit verify first?
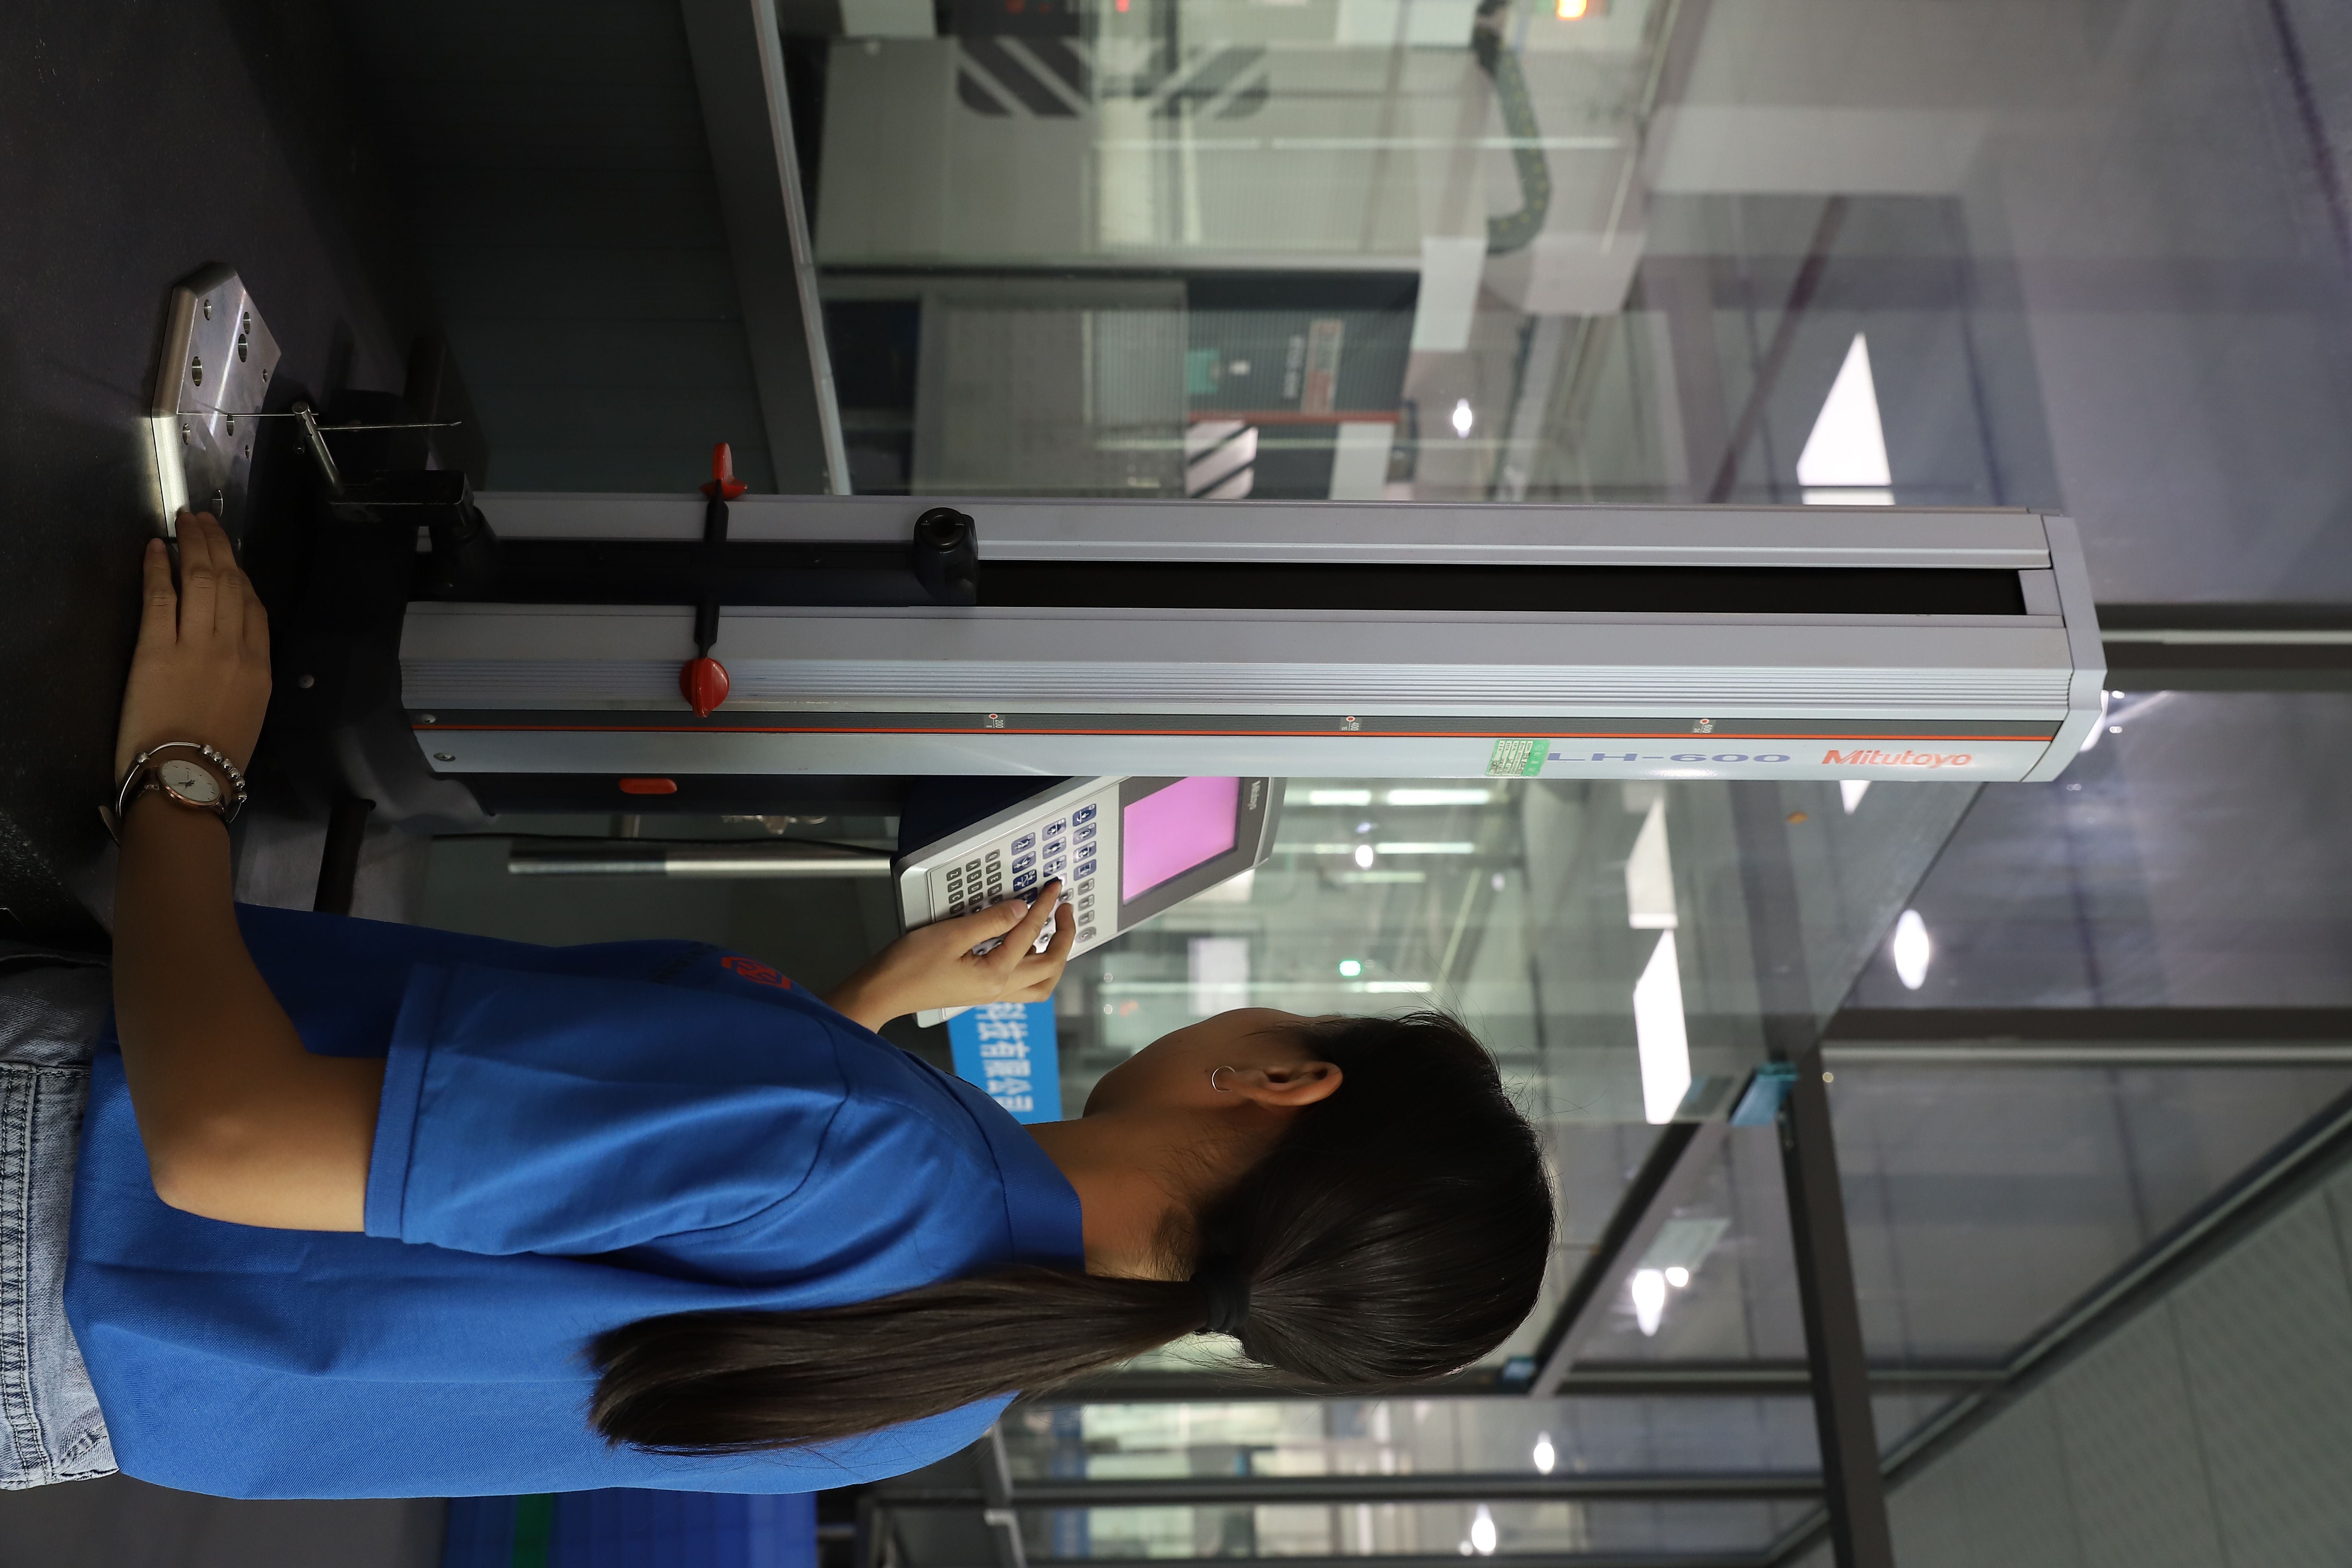
Certifications are the cheapest check because a registrar has already audited the system for you, but only if you verify them. A logo means nothing; the certificate number is what you take to the registrar. The three standards here, with their numbers, are the starting point of any quality audit.
| Standard | Certificate number | Scope (as issued) |
|---|---|---|
| ISO 9001:2015 | 116024/A/0001/UK/En | Machining of metal parts |
| IATF 16949:2016 | 131941/A/0001/SM/En | Manufacture of CNC metal machining parts (excludes product design, Clause 8.3) |
| ISO 14001:2015 | 116024/B/0001/UK/En | Environmental management related to machining of metal parts |
Read the scope, not just the name. IATF 16949 excludes product design under Clause 8.3, which means this is a build-to-print manufacturer. A quality system that states its scope plainly is one you can audit honestly; one that blurs it is hiding something.
How do you verify the measurement equipment and its discipline?

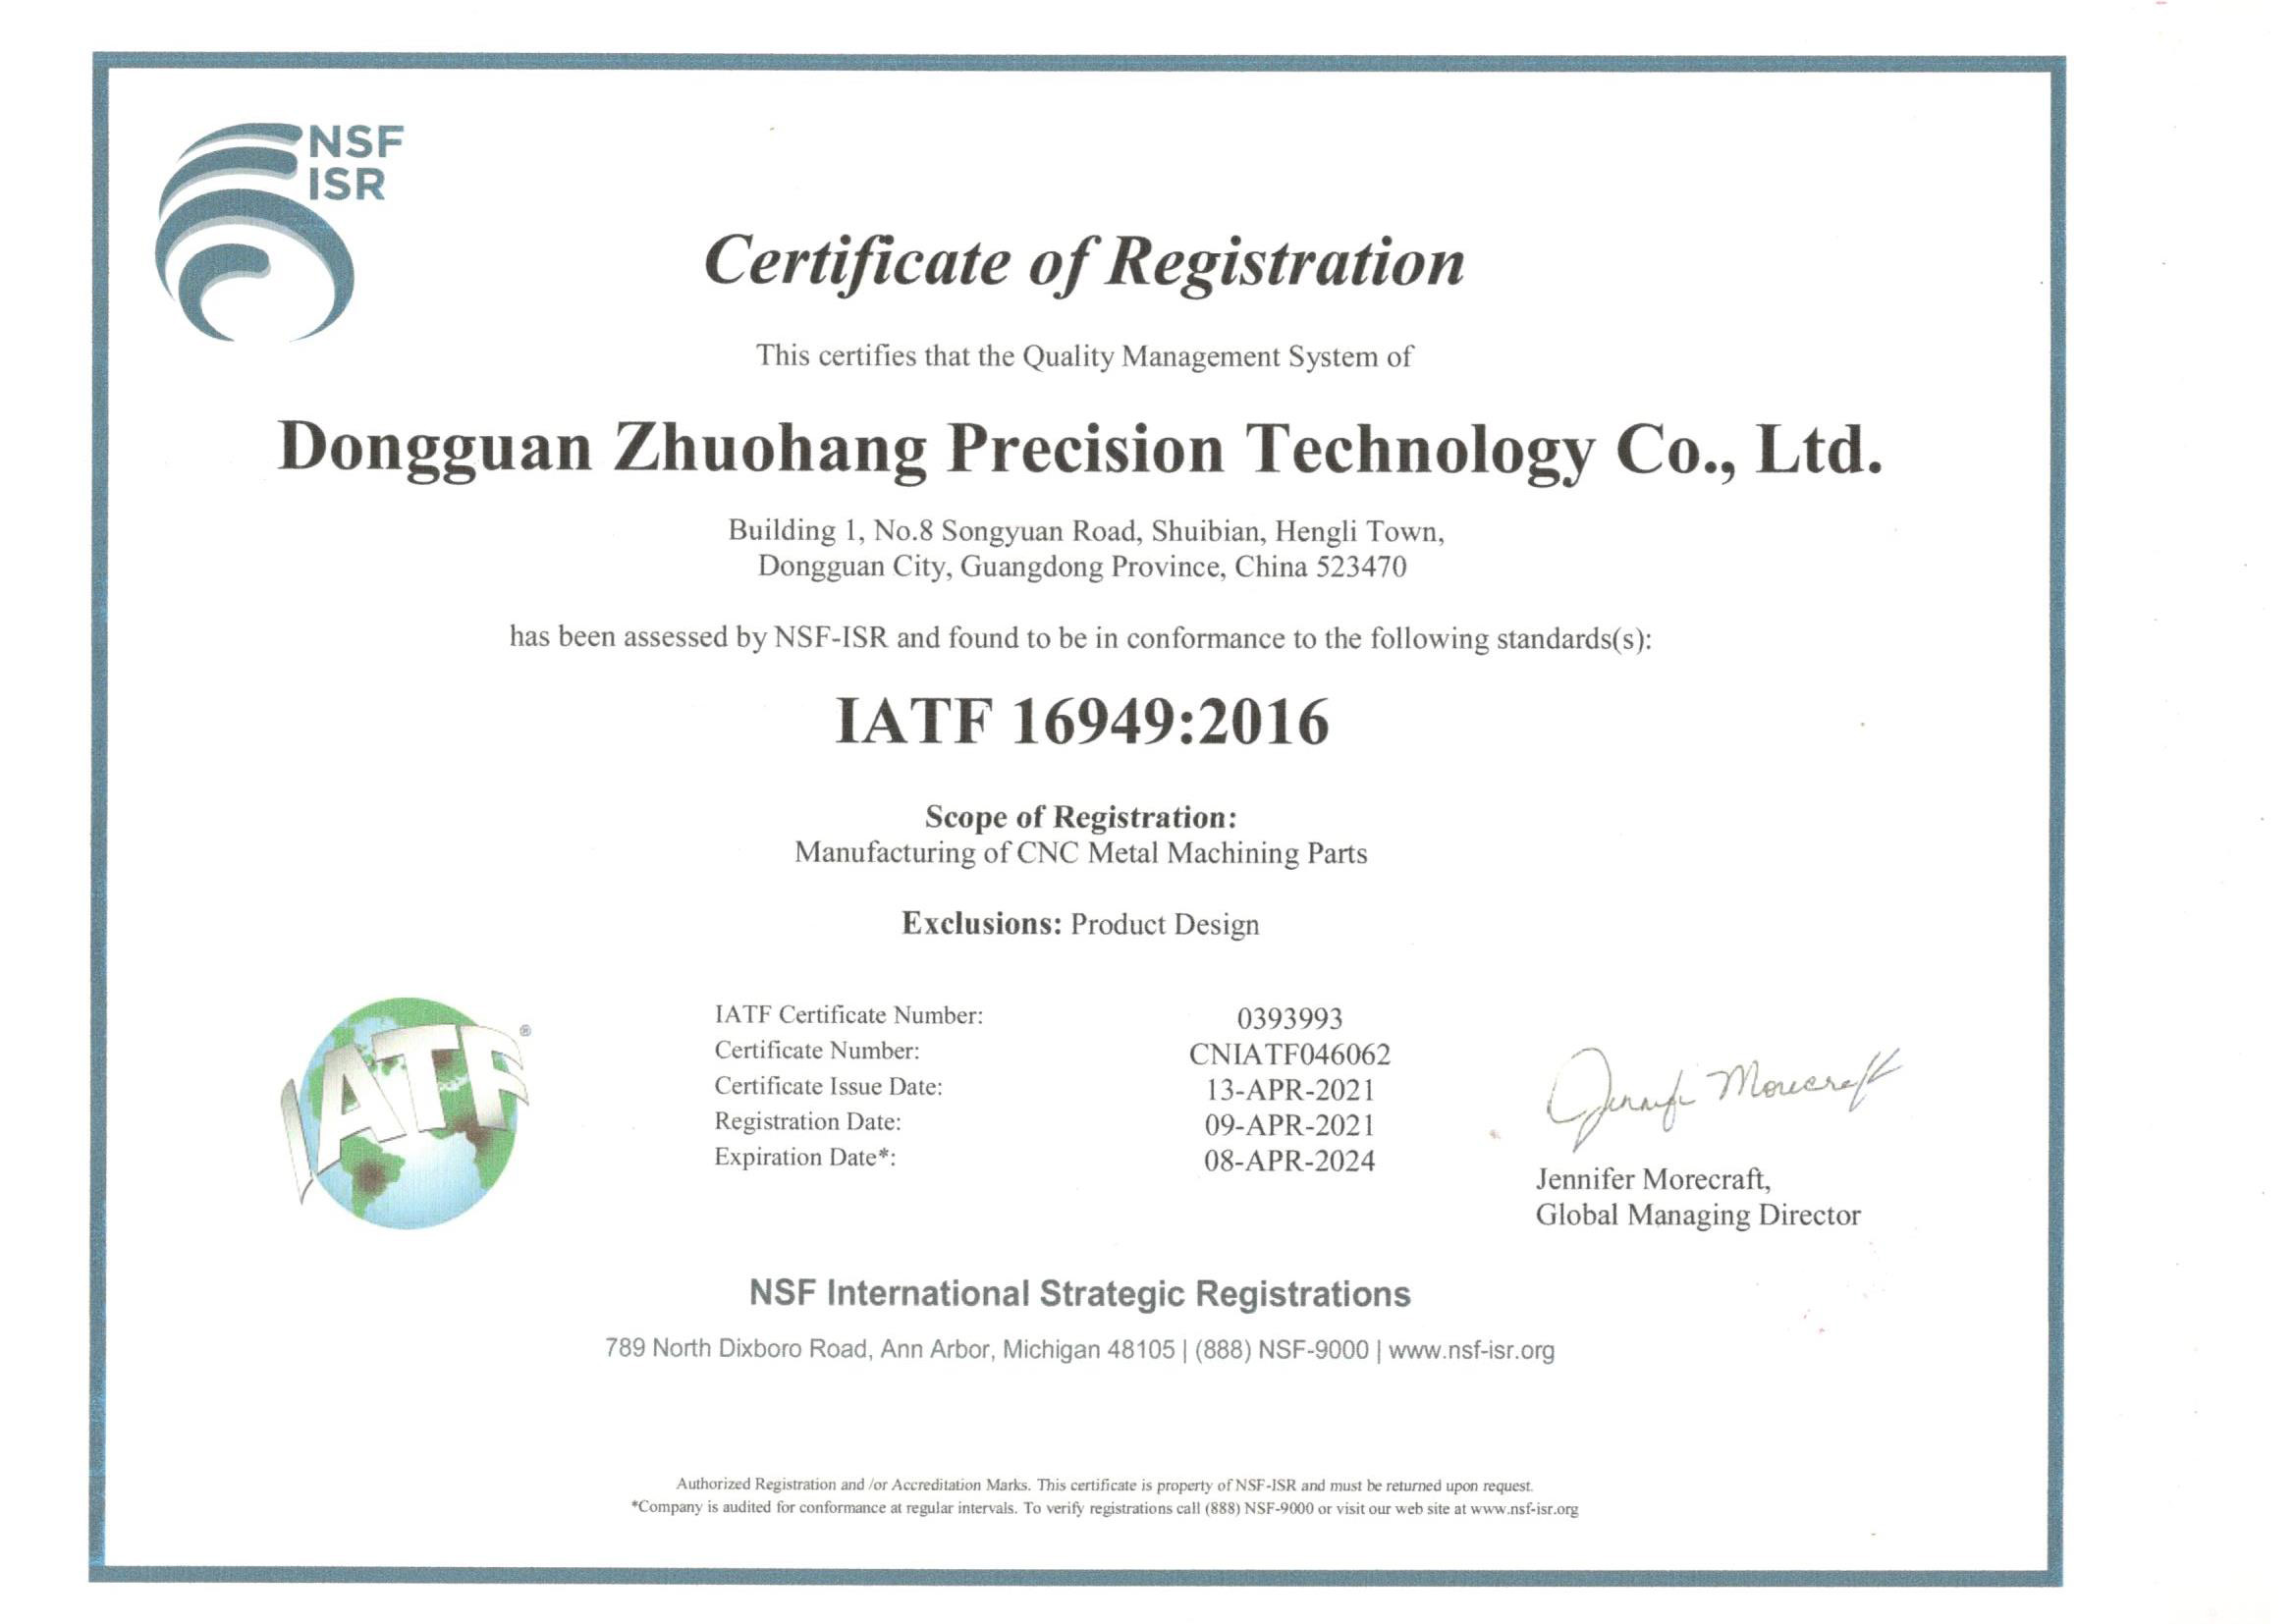
A tolerance is only as real as the instrument that checks it, and metrology has its own uncertainty, so the instrument must be an order of magnitude finer than the feature it verifies. The bench here is the same class of equipment a buyer would use to audit: two Hexagon GLOBAL S CMMs, vision measuring machines, a Keyence VK-X3000 laser microscope, a SURFCOM 1800D surface-roughness profiler, height gauges, an XRF spectrometer for alloy checks, a micro-Vickers hardness tester, and salt-spray and tensile testers.
What does a real SPC program look like on the floor?
One good part proves a machine can cut a shape; statistical process control proves it can hold size across the whole run. The audit asks for a live control chart and its Cpk, because Cpk is the number that says whether the tolerance is actually being held or merely survived on the first piece. The internal standard here is Ppk ≥ 1.67 at the initial study on key characteristics and Cpk ≥ 1.33 on general characteristics.
The evidence is concrete: on a representative length characteristic (76.1–76.5 mm), SPC is charted over 25 subgroups of 4 samples, with X̄ = 76.393 and Cpk = 1.851 (one characteristic on one part, not a blanket capability claim), judged OK. A shop that produces a chart like this is controlling tool wear, heat, and clamping as a closed loop; a shop that cannot is hoping the drift stays inside the band.
Read the tolerance band before you read the index. Cpk is a ratio of the tolerance band to the process spread, not an absolute measure of accuracy. The figure above was recorded on a length characteristic with a 0.4 mm band (76.1–76.5 mm) — wide by design. Hold the same process spread against a ±0.005 mm feature and it fails outright. Ask for the band, the subgroup count and the sampling window on every capability number a supplier quotes.
How do you audit APQP and PPAP capability?

Inspection catches defects; process planning prevents them. The APQP/PPAP package is the evidence that a supplier plans a process before it cuts, and it is exactly what automotive buyers expect to see. The documented package here, on a customer program, includes a process flow chart (incoming inspection through CNC turning, milling, QC, finishing, carburizing, cleaning, and final inspection), a control plan with key characteristics and sampling frequency, a PFMEA with severity, occurrence, and detection ratings, and the SPC charts — plus environmental control procedures for noise, waste water, and air.
When you audit, ask to see a control plan and a PFMEA for a part similar to yours. A supplier that can produce them is doing engineering; one that cannot is doing inspection-only quality, which is a weaker system than the certificate implies.
How do you check traceability across the process?
Traceability is what turns a defect from a mystery into a contained lot. The audit test is to pick a part and ask the supplier to walk it back to its raw material source, process parameters, machine data, batch, machining time, operator, and inspection result. The MES/ERP system here records that full chain on every lot, so the answer is a lookup, not a shrug.
Incoming material closes the other end of the chain: every metal lot is XRF-checked against its mill certificate before it reaches a machine. Traceability plus material verification is the discipline that lets a supplier say "this lot, this machine, this operator" instead of "we think it was sometime last quarter."
How do you audit the quality gate flow from incoming to outgoing?
Quality is not a department at the end of the line; it is a set of gates the part must pass through. The flow to verify is: incoming material inspection, first-article approval, in-process checks at the documented sampling frequency, and final inspection before packaging. Each gate should leave a record, and the records should be available, not promised.
The process flow chart here shows the gates explicitly — incoming inspection, QC after each operation, post-processing checks, and a final outbound inspection before packing. A buyer auditing quality should ask to see the gate records for the last lot shipped, and compare them against the control plan's sampling frequency.
What red flags signal a quality system that only exists on paper?
The difference between a real quality system and a paper one shows up in a few specific failures. Watch for these, because each one means the certificate is doing more work than the process is.
- A certificate number you cannot verify with the registrar, or one that is expired.
- Tolerance claims with no CMM report or SPC chart behind them.
- A first article reported as "pass" with no measured values on the tight features.
- No answer when you ask to trace one part back to its raw material.
- A control plan and PFMEA that cannot be produced for a part similar to yours.
Each of these is a cheap test that runs before you place an order, and together they tell you whether quality is a system or a slogan.
How do you audit calibration and measurement uncertainty?
Even a good CMM is only as trustworthy as its last calibration, and every measurement carries uncertainty that must be a small fraction of the tolerance being checked. The audit asks two things: when was the instrument last calibrated, and how does the shop account for measurement uncertainty on a tight feature. A quality system that cannot answer both is relying on instruments it does not truly control.
The metrology here is run in a controlled area, with the instruments — the Hexagon GLOBAL S CMMs, the vision machines, the Keyence laser microscope, and the SURFCOM profiler — kept calibrated and used at a reference temperature, because measuring a warm part in an unstable room measures the room, not the part. Calibration records and the measurement uncertainty on critical dimensions are available on request, so you can see the number behind the number.
How do you audit measurement system analysis and Gage R&R?
A CMM is only as good as the measurement system around it, and measurement system analysis (MSA) is the discipline that proves the gauge, the operator, and the part are all contributing what they should. The core tool is Gage R&R — repeatability and reproducibility — which separates the variation that comes from the measuring itself from the variation that comes from the part.
The logic is worth understanding because it is the same logic as process control, applied one level down. Repeatability is whether the same operator and the same gauge give the same reading on the same part, again and again. Reproducibility is whether two different operators agree. If a Gage R&R study shows the measurement system contributes little of the total variation, the measurements can be trusted to judge the process; if it shows the gauge or the operator is the dominant source of variation, then the shop is measuring noise, not parts. The common acceptance band is that a measurement system contributing under 10% of the total variation is acceptable, between 10% and 30% is marginal and needs justification, and above 30% is not acceptable for controlling a tight tolerance.
The audit question is simpler than the math: does the shop run MSA on the instruments that check your critical dimensions, and can it show the study? A quality system that documents Gage R&R on its CMMs is proving the number behind the number; one that has never run the study is reporting readings it has never validated. The same question extends to the operators — a gauge used by ten people with no agreement study is a gauge that produces ten different truths.
What are the PPAP levels, and which does your program need?
Production Part Approval Process (PPAP) is the automotive industry's standardized way of proving a supplier can make a part consistently before volume starts, and it comes in levels that define how much evidence the customer receives. The level is a scope decision you make with the supplier, and the audit question is whether the shop can produce the level your program requires, not just whether it has heard of PPAP.
- Level 1: the supplier submits the part submission warrant only, with the supporting data held at the supplier's location.
- Level 2: the warrant plus product samples and a limited set of supporting data are submitted to the customer.
- Level 3: the warrant, product samples, and the complete supporting data package are submitted — the level most automotive customers default to.
- Level 4: the warrant and any other items the customer specifies, with the rest of the package held at the supplier.
- Level 5: the warrant, product samples, and the complete package are available for review at the supplier's location.
The package itself is what tells you the shop plans its process rather than just inspecting its output: a process flow chart, a control plan with key characteristics and sampling frequency, a PFMEA with severity, occurrence, and detection ratings, dimensional results, material and performance test results, and the SPC charts. This facility documents that package on a customer program, with the process flow running from incoming inspection through CNC turning, milling, QC, finishing, carburizing, cleaning, and final inspection.
When you audit, the useful move is to ask for a control plan and a PFMEA for a part similar to yours, at the level your program specifies. A supplier that can produce them is doing process engineering; one that cannot is doing inspection-only quality, which is a weaker system than the certificate implies. The level you request is a business call; the ability to produce the package behind it is the technical fact the audit is there to confirm.
What this shop actually runs
Capability evidence should come as specifics, not slogans. Behind this guide is a 6,800 m2 plant in Dongguan, China running 100+ CNC machines with 100+ staff. The machine list by category:
- 5-axis machining centres (10+) - Mazak VARIAXIS I-600 (510/910/510 mm travel, 12,000 rpm, 22 kW, 71.6 N·m, 30-tool BT40) and Mazak INTEGREX I-250H S (B-axis 0.0001°, 24 kW, 124 N·m, 38-tool HSK-A63). Intended for compound-angle parts, single-setup multi-face prismatic work, and aerospace fittings where datum transfer loss is unacceptable.
- 3-axis / 4-axis machining centres (50+) - Brother SPEEDIO S500Z2N / S700Z2N (10,000 rpm, 14/21-tool ATC, 0.7 s tool-to-tool, Z-axis 2.2 G) and Mazak VCE-430A L / VCE-570C L (10,000 rpm, 118 N·m, 24-tool ATC). Intended for prismatic parts, plates, brackets, housings.
- Swiss-type turning centres (10+) - Citizen Cincom A20-3F7 (Φ20 mm, 10,000 rpm), TSUGAMI B0206-III / B0205-III (Φ20 mm, 0.1 µm), STAR SR-32JII / SR-32J Type N (Φ32 mm, 8,000 rpm). Intended for long, slender rotational parts at ±0.002 mm.
- CNC turning centres (20+) - HEADMAN T70M/1250 (720 mm swing, 117 mm bore, 3,000 rpm, BMT75 12-station turret). Intended for shafts, bushings, flanges up to ±0.002 mm.
- Wire EDM (5+) - Sodick AQ535L (550/350/300 mm travel, ±20° taper, 800 kg workpiece). Intended for hardened tool steel, internal splines, sharp internal corners that milling cannot reach.
- Inspection: Hexagon CMM + 20+ gauges - Hexagon CMM for coordinate measurement, plus vision system, profilometer, hardness tester, coating thickness gauge, XRF for material verification. The 10:1 rule (gauge 10x more accurate than the band) is applied to every feature.
- Machine highlights - VARIAXIS I-600: one-setup multi-face 5-axis + MAZA-CHECK auto-calibration; INTEGREX I-250H S: DONE-IN-ONE mill-turn, B-axis 0.0001° + Ai thermal shield; SPEEDIO S500Z2N / S700Z2N: Z-axis 2.2 G + 0.7 s ATC; Swiss-type: guide-bush switchable + 0.1 µm resolution.
Tolerance: ±0.003 mm CNC milling / ±0.002 mm CNC turning / ±0.002 mm grinding and wire EDM. Capability: Ppk >= 1.67 initial on key characteristics, Cpk >= 1.33 ongoing.
Certificates: ISO 9001:2015 (116024/A/0001/UK/En), IATF 16949:2016 (131941/A/0001/SM/En, with design clause 8.3 excluded, stated openly) and ISO 14001:2015 (116024/B/0001/UK/En), issued to Dongguan Zhuohang Ltd, registration 91441900MA4UWT6X39, founded 2005.
Where we ship: Austria, Belgium, the Czech Republic, Denmark, France, Germany, Greece, Hungary, Ireland, Italy, the Netherlands, Spain, Sweden and the United Kingdom in Europe; Brazil, Canada, Mexico and the United States in the Americas; China, Israel, Japan, Singapore and Sri Lanka in Asia; Australia and New Zealand in Oceania; and South Africa in Africa — plus other countries and regions worldwide, shipped from our base in Dongguan, China.
Contact: Felipe Iglesias, [email protected], +86 13126536955.
Audit the quality system before you order
Request the certificates, a CMM report, and an SPC chart from [email protected] or call +86 13126536955 and see the evidence for yourself.
Frequently Asked Questions
Which certifications back the quality system?
ISO 9001:2015 (116024/A/0001/UK/En), IATF 16949:2016 (131941/A/0001/SM/En), and ISO 14001:2015 (116024/B/0001/UK/En), all issued by URS. IATF 16949 scope excludes product design under Clause 8.3, stated plainly.
What metrology equipment verifies the parts?
Two Hexagon GLOBAL S CMMs, vision measuring machines, a Keyence VK-X3000 laser microscope, a SURFCOM 1800D surface-roughness profiler, height gauges, an XRF spectrometer, a micro-Vickers hardness tester, and salt-spray and tensile testers.
What does the SPC program look like?
In short, Control charts are run on key characteristics, with Ppk ≥ 1.67 initial required on critical characteristics and Cpk ≥ 1.33 on general ones. A representative length characteristic (76.1–76.5 mm) is charted with Cpk = 1.851 (one characteristic on one part, not a blanket capability claim).
Does the quality system include APQP and PPAP?
Yes. A customer program is documented with a process flow chart, control plan, PFMEA, SPC charts, and environmental control procedures — the automotive-grade package that proves process planning, not just inspection.
How is traceability maintained?
The MES/ERP system records raw material source, process parameters, machine data, batch, machining time, operator, and inspection results on every lot, so a single part can be traced end to end on demand.
How is incoming material verified?
Every incoming metal lot is checked by XRF spectrometer against its mill certificate before it reaches a machine, so a mixed or substituted alloy is caught at the door rather than discovered on the finished part.
What red flags signal a paper-only quality system?
In short, A certificate number that cannot be verified, tolerance claims with no CMM report, a first article reported as pass/fail with no measured values, and an inability to trace one part back to its raw material — all signs the system exists on paper only.
How do I request the quality evidence?
Email [email protected] and request the certificates, a CMM report, an SPC chart, and a first-article inspection format before you place an order, so the evidence arrives with the quote, not after the parts.
CNC Machining Precision Quality — Related Pages
Standards referenced on this page
- IATF 16949:2016 — Automotive quality management system standard
- ISO 14001 — Environmental management systems — Requirements with guidance for use
- ASTM A582/A582M-12 — Standard Specification for Free-Machining Stainless Steel Bars